


The Singaporean manufacturing sector is leading in adopting IoT technology to enhance efficiency and stay competitive globally. IoT enables real-time data collection, predictive analytics, and smart automation, helping minimize downtime and optimize resource management.
IoT is transforming traditional manufacturing processes into responsive, data-driven ecosystems. According to Twimbit, the Singapore IoT market is projected to reach $2.9 billion by 2025, growing at a CAGR of 24.92%, driven by the nation’s strong digital infrastructure and adoption of automation.
Nonetheless, how precisely can IoT in manufacturing increase efficiency? The article discusses further its main benefits, which include real-time monitoring, predictive maintenance, supply chain optimization, and energy savings, allowing manufacturers to confidently navigate Industry 4.0.
 Key Takeaways

IoT in manufacturing involves using connected devices, sensors, and software to link machines, tools, and systems within a factory. These systems work together to gather and share data instantly, allowing for automation and reducing the need for manual intervention.
IoT is now widely used across industries, such as manufacturing, healthcare, and smart cities, enhancing decision-making and operational efficiency. By enabling predictive maintenance, supply chain optimization, and smart operations, IoT is reshaping how businesses function in the digital era.
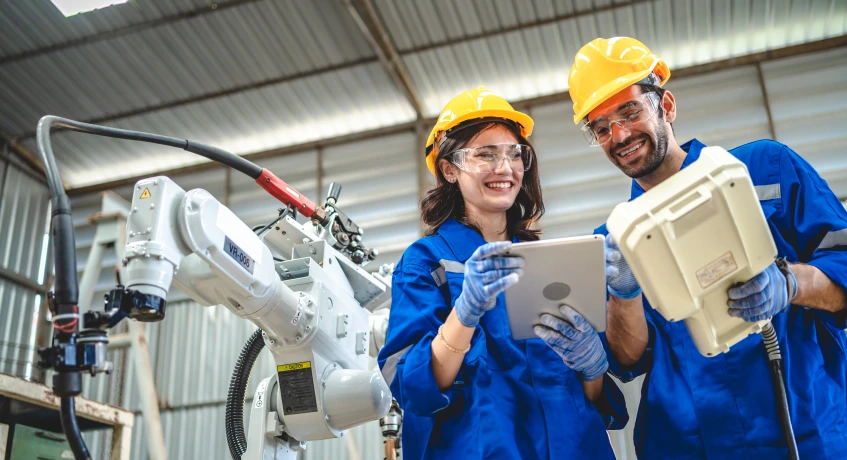
IoT and additive manufacturing are transforming industries by enabling real-time monitoring and efficient production. IoT in manufacturing connects machines, tools, and systems to collect and share data in real-time, making processes more automated and efficient.
By integrating IoT into factory floors and outdoor operations, businesses can boost performance and reduce costs through smart technology and predictive insights. Here’s how IoT is used in manufacturing:
IoT is transforming factory floors by connecting machines and equipment for real-time monitoring and predictive maintenance. Sensors detect issues before they cause breakdowns, helping businesses reduce downtime and keep operations running smoothly.
The same technology extends to outdoor operations, where IoT sensors track equipment and environmental conditions in real time. This integration helps businesses optimize performance by providing valuable insights into maintenance needs, even in remote locations.
Here is an example for predictive maintenance:
IoT is a game-changer for supply chain management by providing real-time tracking of materials from production to delivery. Sensors in products and transport vehicles give businesses visibility into inventory levels, helping optimize routes and avoid delays.
With IoT, manufacturers can easily track their supply chains from start to finish. This not only speeds up decision-making but also improves coordination, reduces waste, and ultimately results in better cost control and more satisfied customers.
Here is an example for supply chain optimization:
IoT makes remote monitoring of machinery and operations possible, allowing managers to oversee multiple processes from a central location. This flexibility ensures quick decision-making and faster responses, even when not physically present at the site.
With IoT, businesses can adjust processes in real time to optimize machine performance. This reduces the need for on-site visits, lowers costs, and enhances overall efficiency, especially when managing operations in remote or spread-out locations.
Here is an example for remote operations:
IoT brings significant advantages to the manufacturing industry, providing enhanced operational efficiency, cost reductions, and improved product quality. By leveraging real-time data, predictive maintenance, and automation, manufacturers can streamline processes and drive long-term success.
Here are the key benefits of IoT in manufacturing:
IoT enables real-time monitoring of equipment, allowing for predictive maintenance and reducing downtime. By automating tasks and optimizing resource management, IoT helps manufacturers improve efficiency and productivity, allowing for faster production cycles.
With IoT, manufacturers can also track the performance of machines and processes more effectively. This data-driven approach helps identify bottlenecks and inefficiencies, leading to continuous improvements in workflows and overall operational performance.
IoT helps manufacturers reduce operational costs by optimizing processes and resource usage. Through real-time data analysis, businesses can identify areas of waste, minimize energy consumption, and avoid costly downtime from unexpected machine failures.
By implementing IoT solutions for predictive maintenance and process automation, manufacturers can also reduce labor costs and increase the lifespan of equipment. This results in long-term savings and a more efficient use of resources.
IoT improves workplace safety by monitoring equipment and environmental conditions in real time. Sensors can detect hazards such as temperature changes, equipment malfunctions, or safety protocol violations, alerting workers and managers immediately to prevent accidents.
In addition to safety equipment, IoT also helps companies enforce compliance with safety regulations. Real-time data helps businesses proactively address potential risks and ensure a safer working environment, reducing injury rates and enhancing employee well-being.
IoT enables manufacturers to monitor production processes with greater precision, ensuring consistent product quality. Real-time data from sensors can help identify quality control issues early in the production cycle, minimizing defects and waste.
By using IoT for quality control, manufacturers can optimize each stage of production and ensure that products meet high standards. This results in fewer errors, better customer satisfaction, and a stronger reputation for quality in the market.
IoT in manufacturing enables businesses to scale operations efficiently. As production demands increase, IoT systems allow companies to seamlessly expand their operations by adding new devices or enhancing existing infrastructure without major disruptions.
By leveraging IoT’s scalable solutions, manufacturers can easily adapt to changing market conditions. Real-time data and automated systems help businesses stay flexible, manage larger volumes of production, and maintain operational efficiency as they grow.
The key benefits of IoT in manufacturing, including improved efficiency, lower costs, better safety, and quality, are crucial for growth. So, ScaleOcean’s manufacturing software seamlessly integrates IoT solutions to optimize operations, enhance monitoring, and support scalability.

Implementing IoT in manufacturing presents challenges, including legacy system integration, data security, and high costs. Overcoming these hurdles requires strategic planning, investment, and skilled expertise to ensure successful adoption and maximize benefits.
Here are a few challenges in implementing IoT in manufacturing:
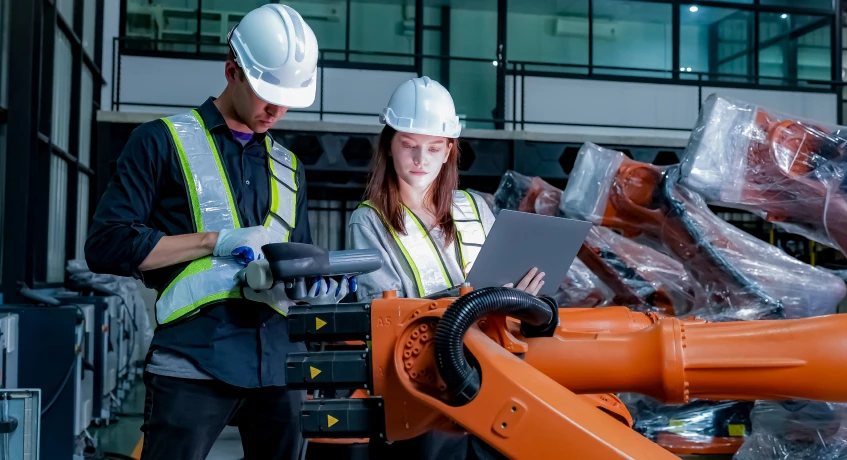
IoT in manufacturing enables real-time monitoring, automation, and predictive maintenance, which improves efficiency and lowers costs. Its applications boost safety, equipment longevity, and reliability, enabling smarter, sustainable production.
Here are the main applications of IoT in manufacturing:
IoT in manufacturing is evolving with AI analytics, 5G, and blockchain, enhancing connectivity, security, and real-time decision-making. The following manufacturing industry trends drive efficiency and innovation, helping manufacturers stay competitive.
Here are the latest trends in IoT for manufacturing:
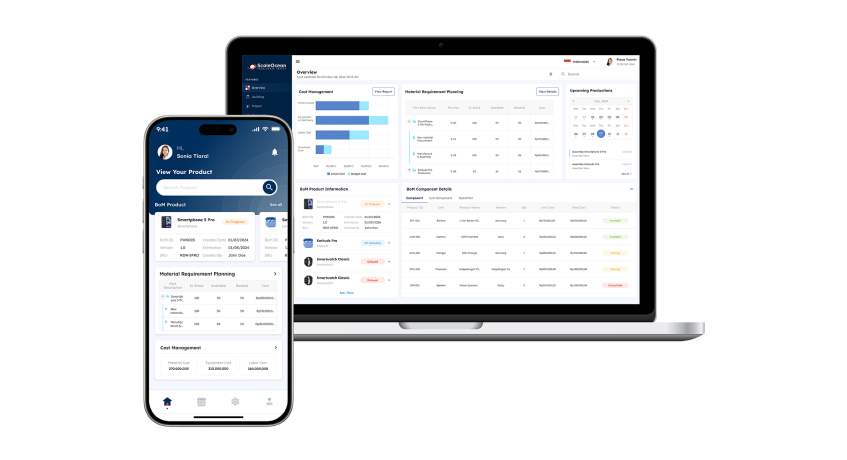
ScaleOcean’s manufacturing IoT solution is a trusted software designed to meet the evolving needs of the manufacturing industry through IoT-driven technology. By integrating smart technology with advanced analytics, it empowers manufacturing businesses to optimize production, reduce inefficiencies, and foster innovation.
Whether you are seeking to enhance real-time visibility, streamline workflows, or improve predictive maintenance, ScaleOcean offers intelligent solutions that elevate your operations.
In addition, ScaleOcean helps companies lower operational costs by improving resource allocation and minimizing downtime. With the CTC grant, businesses can receive financial support to implement ScaleOcean’s solutions, helping them achieve smarter and more efficient production without the financial burden.
Key Features:
ScaleOcean’s IoT solutions help Singaporean manufacturers stay competitive by aligning with smart industry initiatives. By using real-time data, predictive maintenance, and seamless connections, businesses can boost productivity, ensure compliance, and strengthen their supply chain.
IoT is transforming manufacturing by boosting efficiency, improving productivity, and cutting costs. While it offers significant benefits, businesses must address challenges like cybersecurity, integration, and data management to fully unlock its potential.
As technology evolves, ScaleOcean’s Manufacturing solution will help businesses create smarter, more connected production environments. To experience its benefits firsthand, try ScaleOcean’s free demo and take the first step toward optimizing your manufacturing processes.
As more businesses adopt IIoT, the IoT-enabled digital thread is becoming a key trend in manufacturing. IIoT sensors provide real-time data from machinery and processes, ensuring that accurate and up-to-date information flows smoothly across all production stages.
The IoT system is structured across four layers, which include the physical layer, network layer, middleware layer, and application layer. These layers work together to capture, analyze, process data, and recommend actions using advanced software and applications.
IoT can be divided into four main types, which are Consumer IoT, Commercial IoT, Industrial IoT, and Infrastructure IoT. Each type serves a unique purpose, from improving daily life to optimizing industrial operations and managing city infrastructure.
The first five C’s, which are connectivity, continuity, compliance, coexistence, and cybersecurity, are crucial for IoT success. However, the sixth C, customer experience, is what truly sets your device apart from others. Users interact with IoT through software and firmware.